1. Overview
A manufacturer building a new plant to produce 12 m carbon-fibre electric day boats from prepreg — up to 120 boats a year on two assembly lines — invited CoatTech to engineer the paint booth. The plant would paint complete hulls, decks and components in two-component polyurethane, and the booth had to bake at 60 °C.
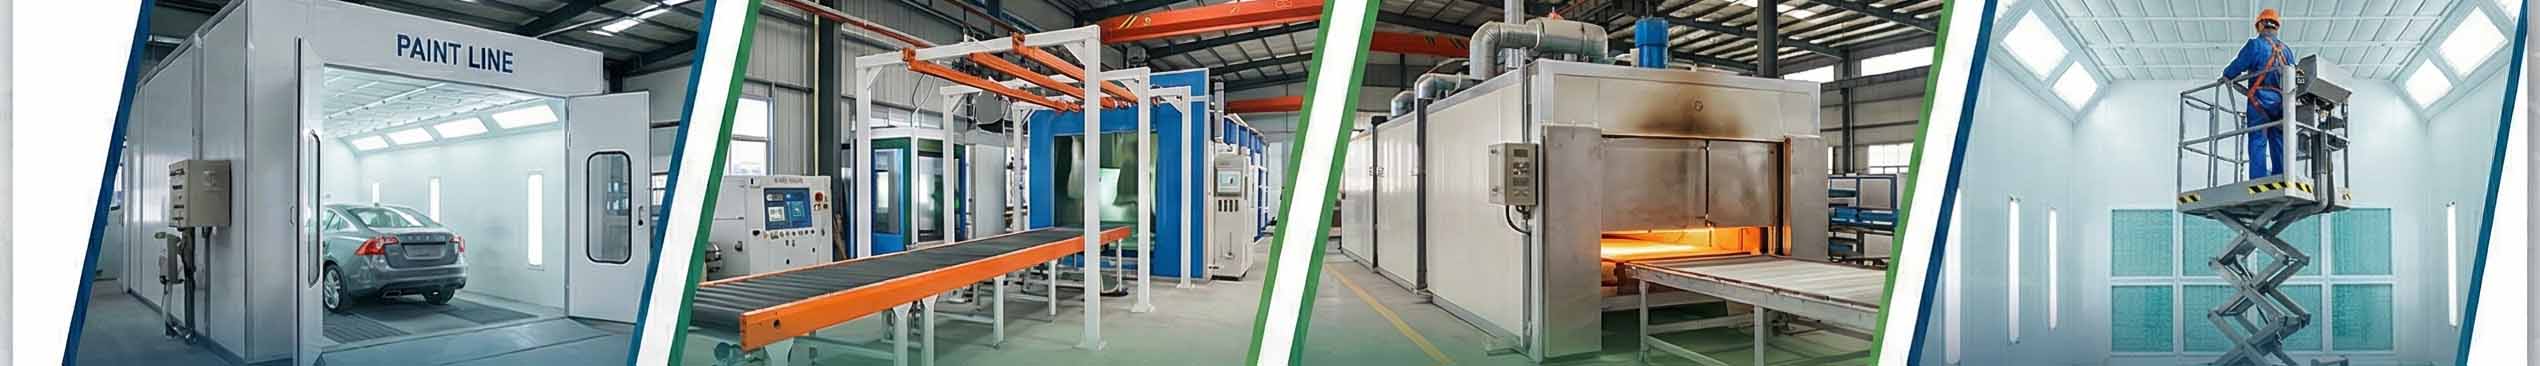
CoatTech delivered a spray and bake booth of 15,000 × 7,000 × 4,000 mm internal, moving 112,000 m³/h across four independently controlled zones, with 264 kW of all-electric heating and 1,000 lux of LED lighting. The engineering interest lies not in the size but in four decisions that shaped the design.
2. Four engineering problems, and how each was solved
2.1 Making all-electric heating affordable at 112,000 m³/h
The client specified electric heating only — no gas, no diesel. Spraying requires 100 % fresh air, which at this size means heating 112,000 m³/h from ambient every minute if the booth runs full fresh air throughout. At a 35 °C intake and a 60 °C setpoint, that single requirement implies roughly 860 kW of heating.
Baking is different from spraying. No paint is being applied, so the only contaminant is the solvent flashing off the film. That makes recirculation safe. CoatTech specified a motorised changeover damper allowing up to 70 % recirculation in bake mode, which cuts the heating demand to roughly 258 kW — about a third. 264 kW of installed heating capacity is sufficient, split into four zones of 66 kW.
|
Mode
|
Fresh air
|
Heating demand at 60 °C (35 °C intake)
|
|
Spraying
|
100 %
|
Not applicable — no heating during spraying
|
|
Baking, full fresh air
|
100 %
|
approximately 860 kW
|
|
Baking, 70 % recirculation
|
30 %
|
approximately 258 kW
|
2.2 Holding VOC face velocity inside the 1.2 m/s limit
Each exhaust cabinet handles 28,000 m³/h, or 7.78 m³/s. The first carbon sizing — 0.507 m³ per cabinet, laid one brick deep at 100 mm — gave a face area of 5.07 m² and therefore a face velocity of 1.53 m/s. Honeycomb activated carbon should not run above 1.2 m/s; above that, residence time falls and adsorption efficiency drops.
The correction is arithmetically simple: 7.78 ÷ 1.2 requires 6.5 m² of face area. CoatTech increased the bed to 0.702 m³ per cabinet, giving 7.02 m² and a face velocity of 1.11 m/s — inside the limit with margin. A temperature probe was added to every carbon box, because activated carbon releases heat when it adsorbs solvent and sustained temperature rise in a carbon bed is a genuine ignition risk.
|
Parameter
|
First sizing
|
Corrected sizing
|
|
Carbon per cabinet
|
0.507 m³
|
0.702 m³
|
|
Face area (100 mm deep)
|
5.07 m²
|
7.02 m²
|
|
Face velocity
|
1.53 m/s — above limit
|
1.11 m/s — within 1.2 m/s limit
|
|
Annual replacement
|
12.2 m³
|
approximately 11.2 m³ per year cycle
|
2.3 Managing the risk that recirculation creates
Recirculation saves energy but it accumulates solvent. With 70 % of the air looping through the booth in bake mode, concentration rises unless it is monitored. CoatTech specified an LEL sensor — one controller with three probes — interlocked so that at 25 % LEL the system alarms, stops the heating and opens full fresh-air ventilation to purge.
The same logic governs the heater itself. The client set the rule: if element surface temperature exceeds 93 °C, the heater must be explosion-proof. 93 °C is the working limit derived from solvent auto-ignition temperature with a safety margin. CoatTech's standard tubular elements run above 100 °C, so the bake circuit is supplied with explosion-proof heaters rather than the standard pattern.
2.4 Humidity: the failure mode that cooling was there to prevent
Two-component polyurethane hardens by reaction with an isocyanate hardener, and that hardener also reacts with water. The reaction releases CO₂, and the film shows it as blushing, pinholing and loss of gloss. In a coastal Gulf location this is a live risk, not a theoretical one.
The client resolved it at plant level: the booth stands inside an air-conditioned production hall, so CoatTech removed air-make-up cooling from scope rather than sell capacity that would not be used. That reduced both capital cost and connected load. The engineering consequence is worth stating plainly, because it is the point most often missed: the booth discharges the full 112,000 m³/h to outdoors in spray mode, so the hall air-conditioning must replace that air continuously. Cooling is not eliminated — it is moved. CoatTech raised this with the client as a design check rather than leaving it implicit.
3. Why composite hulls need a different booth
This is the part of the project that generalises to other composite work, and it is where most steel-derived specifications go wrong.
|
Composite boat hull
|
What the booth must do differently
|
|
Long and low, not tall
|
12 m of clear length but only about 2 m of height. Side-downdraft with raised side plenums delivers the required velocity without excavating a floor pit — a significant civil cost saving on a new build.
|
|
Bake temperature limited by the resin
|
Prepreg systems have a glass transition temperature. Baking above it distorts the hull. Marine composite booths commonly bake at 60 °C rather than the 80 °C and above that steel tolerates. Confirm the resin limit before fixing the setpoint.
|
|
Painted for appearance
|
On most composite boats the fibre is the finish, or the clear coat over it is. Dust and overspray landing on wet clear coat cannot be polished out without losing gloss. Full-ceiling F5 filtration matters more than it would for a protective coating.
|
|
Moisture-sensitive chemistry
|
Two-component polyurethane reacts with water. Cooling alone does not solve it; the air must be brought below its dew point, which is why chilled water at about 7 °C is specified rather than merely cool water.
|
|
Curved, hard-to-light surfaces
|
The lower hull sides and the bow flare are where defects hide, because ceiling lighting throws light past them. Side-wall lighting rows and 3D trolleys are required, and the trolleys must be designed into the booth width from the start.
|
4. Frequently asked questions
|
Question
|
Answer
|
|
How much air does a 15 m boat paint booth need?
|
Multiply the floor area by the required air speed. A 15 × 7 m booth at 0.30 m/s needs about 113,000 m³/h. CoatTech supplied 112,000 m³/h across four cabinets. This single figure drives fan size, duct size, filter area, heating capacity and running cost, so it should be settled early.
|
|
Can a booth this size run on electric heating only?
|
Yes, but only with a changeover damper that permits recirculation in bake mode. Heating 112,000 m³/h of fresh air to 60 °C implies roughly 860 kW. At 70 % recirculation the demand falls to about 258 kW. Without recirculation, all-electric heating at this scale is impractical.
|
|
What face velocity should activated carbon run at?
|
Not above 1.2 m/s for honeycomb carbon. Divide the volumetric flow by the face area: at 7.78 m³/s, 6.5 m² is the minimum for a single cabinet. Higher velocity reduces residence time and adsorption efficiency.
|
|
Why does the heater need to be explosion-proof?
|
Because solvent vapour can ignite on a hot surface without any spark. The working limit is 93 °C, derived from solvent auto-ignition temperature with a safety margin. Standard tubular heating elements run well above this, so heaters in the bake circuit are supplied explosion-proof.
|
|
Does removing cooling remove the cooling load?
|
No. It moves it. A booth in spray mode runs 100 % fresh air and discharges it to outdoors, so whatever conditions the hall must replace that volume. If the booth stands in an air-conditioned hall, the hall system carries the load. The saving is real but it is a transfer, not an elimination.
|
|
Why does humidity matter with two-component polyurethane?
|
The isocyanate hardener reacts with water and releases CO₂, producing blushing, pinholing and loss of gloss. It is one of the most common causes of rework in marine finishing, and it is far more likely in coastal or humid climates. The design relative humidity should be stated in writing in the specification.
|
|
How is a hull moved through the booth?
|
On a transport cradle running on floor rails. The door opening must clear the cradle, not the hull — a 5 × 3 m opening is typical for a 12 m boat. The rail gauge and wheel loads have to be settled before the slab is poured.
|
|
What lighting does a boat hull need?
|
At least 1,000 lux with CRI 90 or better, but the number alone is not enough. Ceiling rows leave the lower hull sides and the bow flare in shadow. Side-wall lighting rows are required for those surfaces.
|

 Your message must be between 20-3,000 characters!